METTLER TOLEDO Introduces M50 R-Series AdvancedLine Metal Detectors
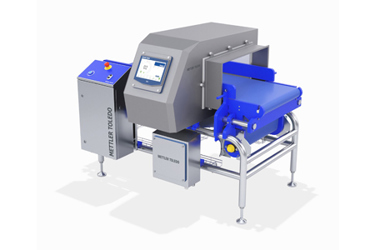
September 15, 2026 - METTLER TOLEDO Product Inspection Group introduces its M50 R-Series AdvancedLine metal detectors to North America at Pack Expo booth 2122. This advanced generation of metal detectors is designed to support food manufacturers facing increasing demands around compliance, traceability, data connectivity and line performance.
"The launch of the M50 R-Series reflects how closely we have listened to our customers. We understand the pressures that food manufacturers face every day: balancing productivity with growing expectations around compliance, traceability and digital connectivity. As production lines become faster and more complex, maintaining that balance becomes even more challenging," said Jaison Anand, Market Manager - Metal Detection at METTLER TOLEDO Product Inspection. "The M50 R-Series has been developed to help address these challenges, delivering advanced detection performance alongside intuitive operation and future-ready connectivity, supporting manufacturers not only today but as their requirements continue to evolve."
The M50 R-Series introduces a range of new innovations developed to increase detection sensitivity and support product safety across different applications. These include the eDrive PLUS, which, when combined with a 900 kHz frequency, improves the field strength to deliver the highest sensitivity to detect the smallest wire and non-spherical metal contaminants. Cutting-edge algorithms such as the 3S PLUS combined with AI-based machine learning help achieve maximum sensitivity, minimizing the risk of product recalls and helping manufacturers produce safer products.
Metal detectors in the series include:
- M55R – Optimized for detecting significantly smaller, irregularly shaped metal contaminants in dry products such as pasta, savory snacks and deep-frozen produce (where thawing does not occur).
- M55RB – Optimized for bulk products such as large sacks, bags of powder and cartons. Radio frequency interference (RFI) shields filter out external interference in large-aperture applications, increasing metal detection sensitivity. The innovative coil geometry delivers consistent detection performance in busy production environments.
- M56R – Optimized for challenging applications such as chilled, wet, dry, deep-frozen/thawing and metalized film-wrapped products. It incorporates multi-simultaneous frequencies, an enhanced 3S PLUS algorithm to minimize the active product signal and an AI-based machine learning process to improve sensitivity on wet or conductive products and virtually eliminate false rejects. The inclusion of a 900 kHz tuned frequency provides excellent performance on dry products, making it a highly versatile solution for manufacturers with diverse products on the line.
The M50 R-Series has been designed to maximize uptime and simplify daily operation. A new 10.1-inch capacitive touchscreen provides clear visualization and intuitive navigation. The interface responds like a smartphone or tablet screen, even when the user is wearing gloves or the screen is wet, to support faster setup and more confident use than traditional resistive touchscreens.
The introduction of the INFINITY Electronic Test System represents a significant advancement in routine testing. Automation in production performance monitoring simplifies test routines, improves consistency and accuracy and is up to three times faster than manual testing. The M50 R-Series can also run tests automatically without operator intervention.
Embedded Wi-Fi supports secure and simplified connectivity, giving users rapid access to system information through QR code functionality. Combined with improved Condition Monitoring software and simplified data transfer, the M50 R-Series supports continuous operation and reduced disruption on the line.
Brand protection is also enhanced through new radio-frequency identification (RFID) access control, which supports individual user logins and access management for superior security. Detailed access records are stored locally or transferred through multiple communication protocols, including OPC-UA and EtherNet/IP.
Manufacturers have the option to take product safety and data security to the next level by integrating ProdX™ data management software from METTLER TOLEDO. By connecting all METTLER TOLEDO Product Inspection devices, ProdX monitors and records all inspection activities in real time and safely stores the data indefinitely.
About METTLER TOLEDO
The METTLER TOLEDO Product Inspection division designs and manufactures both standard and customized inspection solutions - including metal detectors, x-ray inspection systems, checkweighers, vision smart camera solutions and data management software. They prioritize product safety, brand protection and quality assurance for food, pharmaceutical and chemical brands.
With a focus on driving efficiency and innovation, the company helps food, pharmaceutical and chemical manufacturers inspect every product with confidence. Its systems protect brands, profits and productivity while making it easier to comply with industry and customer requirements.
For more information, please visit: www.mt.com/pi